


 (800) 823-4937
 sales@northernhydraulics.net

How to Rebuild a Hydraulic Cylinder: Repair Steps
June 11, 2026
Rebuilding a hydraulic cylinder means swapping the seals and checking the bore and rod so it holds pressure again. Do it when the cylinder leaks, drifts under load, or the rod is lightly scored, and the barrel and rod are still good. The job is short with the right seal kit and a few tools. Depressurize and clamp the cylinder, pull the gland and rod, strip the old seals, inspect the bore and rod, fit the new kit, then torque it back together and test. This guide walks each step in order. It also covers what to send us when you cannot source the seal kit or the cylinder.
What a cylinder rebuild is and when to do one
A hydraulic cylinder rebuild is a seal swap plus a parts inspection. You open the cylinder, replace every seal in the kit, check the bore and rod for damage, and put it back together. The cylinder is usually worth rebuilding. The costly parts, the barrel and the rod, are still good. Only the seals wear out, and a seal kit costs a fraction of a new cylinder. If a replacement turns out to be the better call, browse the full range on the hydraulic cylinders category.
Rebuild the cylinder when you see worn seals. The signs are oil weeping past the rod, the rod drifting down under load, slow or jerky movement, or a film of oil on the rod. All of those point to a seal failure, which is what a rebuild fixes. First, confirm the barrel and rod can be saved. Light rod scoring polishes out, and a glazed bore hones clean. But a deeply scored rod, a bent rod, or a pitted barrel is past a seal kit. That cylinder needs a replacement or a cross-reference. A double-acting cylinder takes oil on both sides of the piston. It still follows the same rebuild path on both ends.
Tools and the seal kit you need before you start
Get the seal kit before you open the cylinder. The kit has to match your bore, rod diameter, and seal cross-sections. Confirm those off the cylinder or the old part number first. Our guide to finding the right seal kit for a hydraulic cylinder walks the cross-reference. The seal-kit cross-reference table below lists what to measure. With the kit in hand, set out the tools.
| Tool or material | What it is for |
|---|---|
| Hydraulic cylinder seal kit | New seals keyed to your bore and rod. |
| Bench vise with soft jaws, or rod clamps | Holds the barrel and rod without marring them. |
| Spanner or pin wrench, socket set | Backs off a threaded gland or the end-cap bolts. |
| Snap-ring or wire-ring pliers, seal pick | Removes the retainer and lifts old seals out. |
| Seal installation tools (no sharp edges) | Seats new seals square without cutting them. |
| Emery cloth or a cylinder hone | Polishes light rod scoring and breaks bore glaze. |
| Micrometer or calipers | Confirms bore and rod size against the kit. |
| Clean solvent, rags, compressed air | Cleans each part so no grit damages the seals. |
| Clean hydraulic oil or assembly lube | Lubricates seals and bore for smooth assembly. |
| Torque wrench | Tightens the gland to the manufacturer’s spec. |
Hydraulic cylinders hold oil at pressure high enough to inject through skin. That is a serious injury that needs surgery fast. Bleed the system pressure and disconnect the lines before you open the cylinder. Never check for a leak with your hand, and treat any fluid injection as an emergency. See the OSHA bulletin on high-pressure hydraulic system hazards, and the NIH medical reference on high-pressure injection injuries of the hand, before service.
How to rebuild a hydraulic cylinder, step by step
Run these six steps in order. The teardown and reassembly are mirror images. The way the cylinder came apart is the way it goes back together. Work clean, because grit on a new seal is the most common reason a fresh rebuild leaks.

- Depressurize and secure the cylinder. Bleed off all system pressure, disconnect the hoses, and cap the ports. Retract the rod. Then clamp the barrel in soft jaws or rod clamps so it cannot move.
- Remove the gland and pull the rod. Back off the end-cap retainer, then draw the rod and gland straight out of the barrel. The retainer is a threaded gland, a snap ring, or a wire ring. If the end cap is stuck, our guide on how to remove a hydraulic cylinder end cap covers each type.
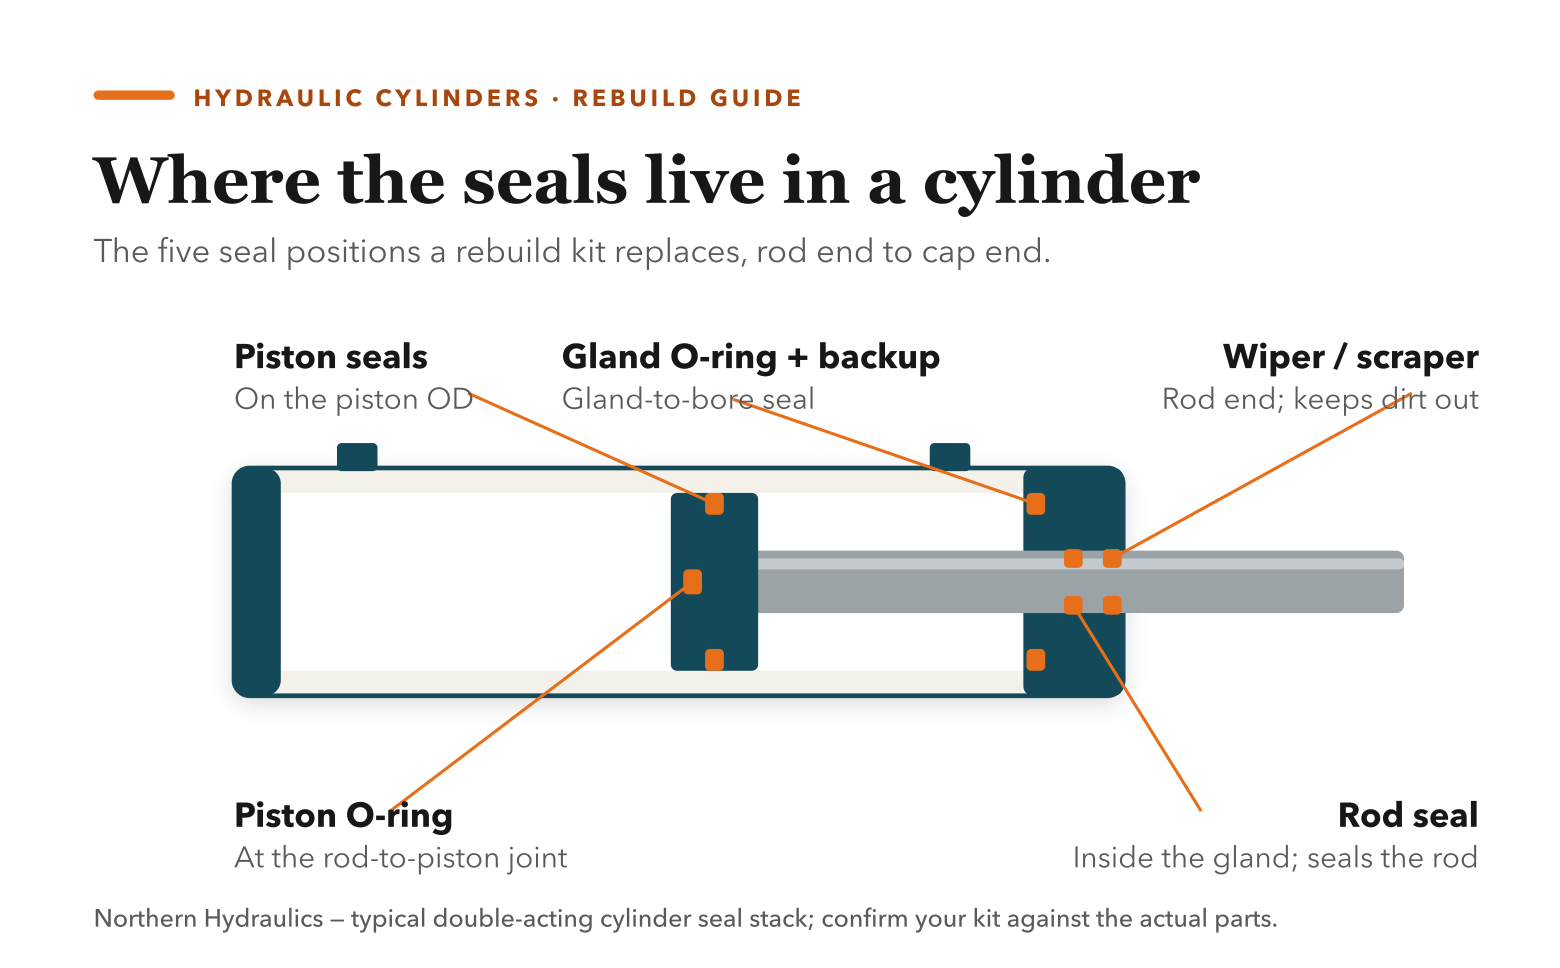
- Strip the old seals. Take the piston off the rod. Then remove every old seal: the piston seals and O-ring, the rod seal and wiper, and the gland O-ring and backup rings. Note which way each seal faces as it comes out. Lay the old seals in order to check the new kit against them.
- Inspect the bore and rod. Clean every part, then look for damage. Polish light rod scoring with emery cloth, and hone a glazed bore smooth. Measure the bore and rod with a micrometer. A bent or deeply scored rod, a pitted barrel, or a worn piston is past a seal kit. Replace that part, or cross-reference the cylinder.
- Install the new seal kit. Lubricate each new seal with clean hydraulic oil. Seat it square in its groove without twisting or stretching it, using a seal tool with no sharp edges. Fit the piston seals and O-ring first. Then fit the rod seal, wiper, and backup rings in the gland, the same way they came out.
- Reassemble, torque, and test. Slide the rod and piston back into the bore so the seals do not catch on the ports. Reseat the gland, and torque it to the manufacturer’s spec. Reconnect the lines, then cycle the rod at low pressure to seat the seals and check for leaks. Bleed any trapped air per our guide on how to bleed a hydraulic cylinder before you put it back to work.
Seal material matters here. Most cylinders run nitrile (Buna-N) seals. Nitrile suits standard petroleum hydraulic oil at normal temperatures. Hotter service or harsh fluids call for fluorocarbon (Viton or FKM) or polyurethane. The wiper and backup rings are often a harder material than the main seals. Match the kit to the fluid and temperature you actually run. Do not swap materials by guess.
Threaded-head, wire-ring, and tie-rod teardown differences
How the cylinder comes apart depends on how the end cap is held. There are three common retainers, and one of them decides most of the teardown.
Choose the threaded-gland path when the gland screws into or onto the barrel. This is common on welded cylinders. Back it off with a spanner or pin wrench in the gland holes. Choose the wire-ring path when a split wire sits in a groove inside the barrel behind the gland. Push the gland in slightly, work the wire out through the slot, then draw the assembly out. Choose the snap-ring path when a retaining ring holds the head. Lift it with snap-ring pliers.
The cylinder type drives the rest. A welded cross-tube cylinder has the barrel welded to the base. You rebuild it from the rod end only, through the gland. A tie-rod cylinder comes fully apart. Unbolt the tie-rod nuts and lift off both end caps. Then you can reach every seal and reface both heads. Tie-rod construction is the easier rebuild. It is why plants standardize on it for machines they service in place.
Seal-kit cross-reference: what to measure to source a kit
The seal kit is the one part you must get exactly right. It cross-references on physical dimensions, not just a part number. If the cylinder is obsolete or unbranded, measure these dimensions off the parts, and our seal-kit cross-reference guide matches a kit to them. Capture each one before you order.
| What to measure | Where to read it | Why the kit depends on it |
|---|---|---|
| Bore diameter | Inside diameter of the barrel. | Sets the piston seal and piston O-ring. |
| Rod diameter | Outside diameter of the rod. | Sets the rod seal and wiper. |
| Seal cross-section | The old seals and their grooves. | A kit can fit the bore but use a different profile. |
| Gland bore and OD | The gland the rod passes through. | Sets the gland O-ring and backup ring. |
| Seal count per groove | The parts as they come out. | Confirms the kit has every piece. |
| OEM and old part number | Stamp on the barrel or the old tag. | Speeds the cross-reference to an equivalent. |
| Working pressure rating | The machine spec or old tag. | Confirms the seal material suits the pressure. |
A cross-reference is a fit guide built on published specs. Verify bore, rod, seal cross-section, and pressure rating against the actual parts before ordering. Can’t source the seal kit or the cylinder? Send us the specs and an NH specialist cross-references it.
If it were our call
For most buyers, rebuild a cylinder that leaks or drifts when the barrel and rod are sound. The seal kit is cheap next to a new unit, and the rebuild is a couple of hours of work. Confirm the bore hones clean and the rod is straight and unscored first. Stop and send us the specs when the rod is bent or deeply scored, the barrel is pitted, or the cylinder is obsolete and the kit is hard to find. We have matched cylinders and seal kits to machines since 1963. We would rather cross-reference the right part than have you rebuild around a worn one. If you would rather not open the cylinder at all, our shop rebuilds it for you, with turnaround estimated after we inspect the unit. Send the bore, rod, and old part number, then browse the cylinder line or request a quote before the machine is down.
Frequently Asked Questions (FAQ)
Short answers to what buyers ask most before rebuilding a hydraulic cylinder.
How hard is it to rebuild a hydraulic cylinder?
It is a manageable bench job for most welded and tie-rod cylinders. You need the right seal kit and a few tools. The work is mechanical, not delicate. Depressurize, pull the gland and rod, swap the seals, inspect the bore and rod, and reassemble. Two things trip people up: getting the end cap off, and seating the new seals square without grit. Go slow on those. If the rod is bent or the bore is pitted, that is past a rebuild, so cross-reference the cylinder instead.
What tools do you need to rebuild a hydraulic cylinder?
You need a seal kit matched to your bore and rod. Add a vise with soft jaws or rod clamps, a spanner or pin wrench, snap-ring or wire-ring pliers, a seal pick, and blunt seal tools. You also need emery cloth or a hone, a micrometer, clean solvent and rags, hydraulic oil, and a torque wrench. The full list is in the tools table above. Confirm the seal kit first against your cylinder.
Is there a diagram for rebuilding a hydraulic cylinder?
Yes. The rebuild sequence diagram above lays out the six steps in order. The cutaway shows where each seal sits, from the rod wiper and rod seal in the gland to the piston seals and O-ring. Use the cutaway to spot every seal a kit replaces. Lay your old seals out in the order you remove them, so the new kit goes back the same way.
What does it cost to rebuild a hydraulic cylinder?
A rebuild is mostly the price of the seal kit plus your labor. That is far less than a new cylinder when the barrel and rod are sound. The kit cost depends on the bore, rod, and seal materials, so it varies by cylinder. We do not quote a flat price sight unseen. Send the specs and we price the seal kit. For a shop rebuild, we estimate it after inspection. Compare against a new unit on the hydraulic cylinders line.
Can I rebuild a double-acting hydraulic cylinder the same way?
Yes. A double-acting cylinder takes oil on both sides of the piston. So it has piston seals that hold pressure both ways, plus the rod seal and wiper. The rebuild path is the same. Pull the rod, replace the piston seals and O-ring along with the rod seal, wiper, and backup rings, then reassemble. Most loader, splitter, and press cylinders are double-acting. Match the full kit from the cross-reference table so you replace every seal, not just the one that failed.
Can you rebuild or cross-reference an obsolete hydraulic cylinder?
Usually, yes. A seal kit cross-references on the bore, rod, seal cross-section, and pressure rating. It does not depend on a discontinued part number. So an obsolete cylinder is often still serviceable. Measure those dimensions, or send the old part number and the cylinder specs. An NH specialist confirms a current seal kit or a replacement cylinder. That cross-reference work is what we do most. Request a quote with the specs to source it.


